Cast iron surface plate maintenance and recalibration schedule
Oct 09,2026
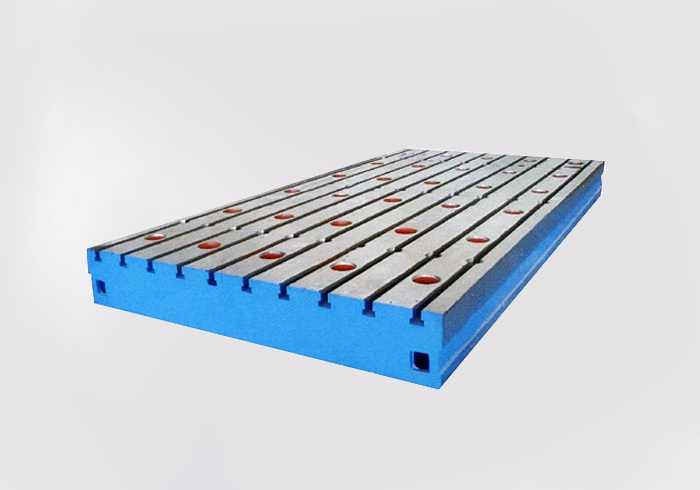
A cast iron surface plate is bought once and expected to hold its accuracy for a decade. Whether it does comes down to three things: how it is levelled, how it is treated between measurements, and whether anyone actually keeps the recalibration date. This guide sets out the routine, and the intervals.
Why a plate holds its accuracy, or loses it
A scraped cast iron plate does not lose accuracy because it wears out. It loses accuracy because something pushes it out of shape: an uneven support pattern that keeps loading the same points, a workpiece left on the face for weeks, a plate parked next to a heat source, or a face that has been allowed to corrode.
That is the whole reason the maintenance routine matters more than the purchase specification. Two identical plates, treated differently for five years, will not be interchangeable.
Before use: cleaning and temperature
- Clean the anti-rust oil off the working surface with non-corrosive petrol, then wipe the face with degreased cotton yarn before use.
- Work in the 20±5 °C range. Temperature change produces measurement error, and a plate that is stable at 20 °C is not stable at 32 °C.
- Check that the plate is level and that every support point carries an even share of the load. A support that is not touching, or one that is carrying too much, bends the plate.
Setting up and re-levelling
The standard method is three-point levelling, and it is worth doing properly:
- Place three adjustable levelling wedges under three support positions on the underside.
- Put a frame-type precision level on the plate and read it in the longitudinal, transverse and diagonal directions.
- Wherever a reading is outside the tolerance, turn the wedge at that point slightly to raise or lower it.
- Measure and adjust again until every reading is inside the specified tolerance.
Two details are routinely missed:
- Plates longer than 2 m need auxiliary supports in addition to the three main points. An auxiliary support should only touch the underside lightly. If it is forced up, it bends the very face it is meant to protect.
- Tighten the lock nuts once the adjustment is finished. For a newly installed or relocated plate, re-check the levelling once a week for the first month; after that, move to the normal recalibration interval.
After use: protection and storage
- Wipe the plate clean, coat the face with a water-free acidic-free anti-rust oil, cover it with moisture-proof paper and store it in a clean, dry place.
- Take the workpiece off the plate when the job is finished. A heavy workpiece left in place for a long period loads the same area continuously and deforms the plate.
- Keep the plate away from heat sources, corrosive gases and corrosive liquids. Store it in a ventilated, dry area rather than against a wall in a damp corner.
- Handle it carefully. Impact damage to a plate is not something a re-scrape can always fix.
The recalibration schedule
Intervals differ by product, because a plate in a metrology room and a floor rail under a welding bed do not see the same duty cycle.
| Item | Check | Interval |
|---|---|---|
| Cast iron surface plate | Full recalibration | Maximum one year |
| Newly installed or relocated plate | Re-check levelling | Weekly for the first month |
| Cast iron floor rails | Recalibration to standard | 6 to 12 months, depending on duty |
| Levelling wedges under a machine | Condition check and re-levelling if the reading has drifted | Every 3 to 6 months |
The one-year maximum for a plate is a ceiling, not a target. A plate in a busy inspection bay, or one used with heavy workpieces, should be checked on a shorter interval.
What a recalibration actually checks
Recalibration is not a visual inspection. On a scraped plate it includes the contact-point check, and the acceptance limits are worth knowing because they are also what a supplier is judged against:
- The working surface must be free of sand holes, gas holes, cracks, slag inclusions, shrinkage porosity, score marks, bruises and rust spots that would affect appearance or performance.
- On grades 1 to 3, sand holes below 15 mm in diameter may be plugged with the same material, provided the plug is softer than the surrounding metal — no more than four per working surface, at least 80 mm apart.
- The face is checked by colour lapping. Any 25×25 mm square must reach the contact-point count for its grade, and the counts between any two 25×25 mm squares must not differ by more than 5 points.
- On a grade 3 scraped surface the maximum permitted surface roughness is Ra 5 µm.
- Flatness is measured against the flatness tolerance table for the grade.
The contact-point and roughness checks are the reason a plate cannot be assessed by eye. Ask for the record, not for an opinion.
The record is part of the routine
A recalibration only has value if it is dated and filed. The practice that keeps a plate trustworthy over a decade is unglamorous: a log per plate holding the date, the instrument used, the readings and who signed it off.
With that record, a drift of a few microns per year becomes visible while it is still cheap to correct by re-scraping. Without it, the first sign of a problem is a batch of parts that will not gauge, and by then the question is no longer maintenance.
Frequently asked questions
How often does a cast iron surface plate need recalibrating?
At least once a year as a maximum. A plate in heavy or high-precision use should be checked more often, and any plate that has been moved, dropped or re-installed should be checked before it goes back into service.
Does a cast iron plate wear out?
Not in the way a bearing wears out. Accuracy is lost through uneven loading, deformation from a workpiece left in place, thermal effects and corrosion — which is why the routine around the plate matters more than its age.
My plate reads low in one corner. Can I just adjust the wedges?
Check whether the support pattern is the problem before touching the plate itself. An auxiliary support that has been forced up, or a support that has settled, usually explains a local reading. If the plate is still out after levelling, it needs re-scraping, not shimming.
Can a plate that has been re-levelled go straight back into inspection work?
Not on the reading alone. A newly installed or relocated plate should have its levelling re-checked weekly for the first month, because a support that settles will move the reading again.
Does maintenance affect the warranty or the grade?
It affects whether the plate still meets its grade. The acceptance clauses — the plug limits, the contact-point density and the flatness tolerance — are what the grade means in practice, and they only stay true if the plate is checked on schedule.
Need a plate checked, re-scraped or replaced?
Hebei Yuanpeng Machine Tool and Measuring Implement Co., Ltd. has produced cast iron surface plates, machine tool castings and measuring tools since 1995. We hold the national plate measuring tool production licence and were among the first in the industry to obtain ISO 9001 certification. Our products are exported to the United States, Europe, Japan, South Korea and other markets.
Send the plate size, grade and the reading you are getting to yuanpeng@yepoweldingtables.com, or use the enquiry form on our contact page. We reply within one working day.
Related products: Cast iron platform series · High precision flat cast iron plate · T-slot cast iron platform
Previous Page:

Contact Us
E-mail:
yuanpeng@yepoweldingtables.com
Service Hotline:
+86-19933786909
Address:
Industrial Development Zone, Jiaohe Town, Botou City
Sales Hotline: +86-19933786909
E-Mail: yuanpeng@yepoweldingtables.com
Address: (Hebei Province, China) Jianshe Road, Jiaohe Town, Botou City, Cangzhou City, Hebei Province


INQUIRY