Cast iron casting defects: gas holes and sand holes
Oct 02,2026
A gas hole and a sand hole are two small defects that decide whether a casting is accepted, repaired or scrapped. They look similar on a machined surface, but they come from opposite ends of the process — one from gas in the metal, one from the mould. This guide covers where each comes from, the controls that prevent them, and how to inspect for them before the casting leaves the foundry.
What the two defects are
Gas holes are voids left behind by gas that was trapped in the molten iron or in the mould cavity and could not escape before the metal solidified. They appear as smooth-walled, often rounded cavities, sometimes clustered, sometimes isolated on a machined face.
Sand holes are cavities caused by moulding sand coming loose and being carried into the casting, or by the mould surface breaking down where the metal touches it. They typically have a rougher wall and often contain sand residue.
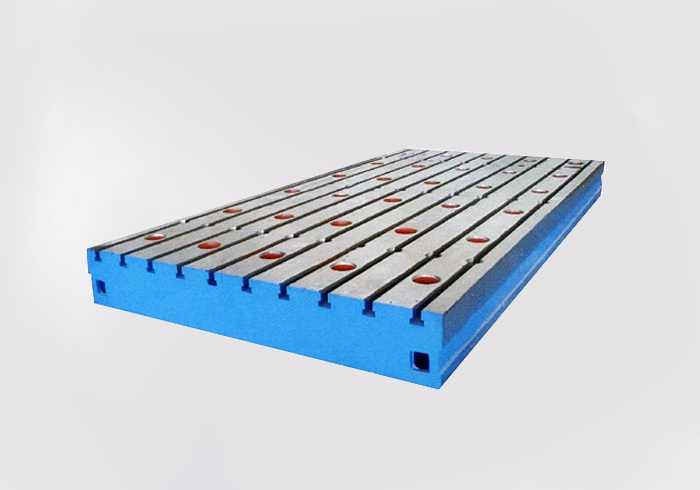
On a cast iron surface plate or platform, both defects land in the same acceptance clause: the working surface must not carry sand holes, gas holes, cracks, slag inclusions, shrinkage porosity, score marks, bruises or rust spots that affect appearance or performance. That is why a foundry's process control matters more to a buyer than the finished surface looks.
Where gas holes come from
Two conditions account for most gas holes in cast iron work:
- Excess gas content in the molten iron. If the melt carries too much gas, that gas has to go somewhere as the casting cools, and it goes into the metal.
- Poor mould venting. Gas generated at the mould face, or air that cannot leave the cavity, has nowhere to go if the mould is not vented properly, so it is pressed into the solidifying surface.
Pouring parameters sit underneath both. A melt or a mould that is otherwise sound will still produce gas defects if the temperature or the pouring speed is outside the working range, because abnormal parameters promote gas evolution at exactly the moment the metal is setting.
Where sand holes come from
Sand holes trace back to the mould rather than the metal:
- Moulding sand quality. Sand that is not up to specification breaks down under the heat and the wash of the pour.
- Sand preparation and ramming. Poor mixing and inconsistent compaction leave weak zones; the surface then scours loose where the metal flows past it.
- Moulding technique. A mould built without consistent technique will have local areas that do not stand up to the pour.
- Parameter excursions. The same abnormal temperature or pouring speed that produces gas defects also promotes sand particles breaking away from the mould face.
Controls in melting and pouring
The measures that actually remove these defects are process measures, not final inspection measures.
| Area | Control |
|---|---|
| Melting | Strengthen degassing in the melt; select a suitable degassing agent |
| Mould design | Optimise the design so the mould vents freely |
| Pouring | Hold pouring temperature and pouring speed within the working range — too high or too low, too fast or too slow, all produce defects |
| Equipment | Maintain and calibrate the key equipment on a schedule — melting furnace, casting machine, and the rest of the line |
| Monitoring | Instrument the process: temperature sensors and pressure monitoring to hold the melting and pouring parameters inside their set range |
The reason equipment condition and live monitoring appear on that list is that parameter excursions, not bad luck, are what drive defects. A furnace that has drifted or a mould that is no longer venting will show up as gas evolution or loose sand in the casting long before anyone notices the equipment itself.
Moulding sand and mould design
Sand-side control is where sand holes are won or lost:
- Select moulding sand that meets specification.
- Control the mixing and the compaction of the sand, and hold it consistently from mould to mould.
- Keep moulding technique consistent across the shop floor — skill is a process variable like any other.
Two moulding methods are worth knowing because they change the defect profile:
Resin sand. A resin-bonded mould has good rigidity and high strength in the early stage of the pour. That stiffness allows the mould to use the graphitisation expansion of the iron as it solidifies, which suppresses shrinkage porosity and shrinkage cavities — and makes low-riser and riserless casting practical for grey and ductile iron.
Lost foam (full-mould) casting. A polystyrene pattern is set in a self-hardening furan resin sand. When the metal is poured, the pattern vaporises and burns away and the metal takes the space the pattern occupied, so the casting reproduces the pattern. For one-off and small-batch work on large parts — machine tool beds being the classic case — this route removes the pattern cost and shortens the cycle, with high dimensional accuracy, small machining allowance and good surface finish.
Mould and core collapsibility belongs on this list too. A mould that cannot give as the casting contracts will tear the casting, so collapsibility is a design decision, not a detail.
Inspection: catching defects before the casting ships
Inspection has to be able to find defects that a visual check cannot:
- Radiographic inspection (X-ray) for internal gas holes and shrinkage.
- Ultrasonic inspection for internal discontinuities in heavier sections.
- Scheduled quality audits of the process itself, not only of the finished casting, so that a drift is corrected rather than re-detected casting after casting.
For cast iron plates and platforms there is also a defined repair window in the standard, and it is narrow:
- Sand holes smaller than 15 mm in diameter may be plugged with the same material, provided the plug is softer than the surrounding metal.
- No more than four plugged holes per working surface.
- Minimum spacing between plugged holes: 80 mm.
- Working surface hardness must still fall inside the specified range after repair.
A plug inside those limits is acceptable. A casting outside them is not, and no amount of surface dressing changes that.
Records and traceability
Defects are cheap to fix at the cause and expensive to fix at the customer. A traceability record per batch — raw material, process parameters, inspection results — is what makes it possible to locate the cause quickly when a defect does appear, instead of guessing.
With that record in place, corrective action is targeted: a change in sand supply, a furnace that needs recalibration, or a pouring practice that drifted are all visible in the data before they become a claim.
Frequently asked questions
What is the difference between a gas hole and a sand hole?
A gas hole is a void left by trapped gas from the melt or the mould cavity; its wall is usually smooth. A sand hole is a cavity caused by moulding sand breaking loose or the mould face breaking down; it is usually rougher and may contain sand.
Can a casting with gas holes or sand holes be repaired?
Small sand holes have a defined repair route on cast iron plates: below 15 mm diameter, plugged with the same material, softer than the surrounding metal, no more than four per working surface and at least 80 mm apart. Defects outside that window are a rejection, not a repair.
Does degassing alone prevent gas holes?
No. Degassing in the melt removes one source of gas, but a mould that does not vent will still trap gas at the surface. Melting control, mould venting, pouring parameters and equipment condition have to hold together.
How are gas holes and sand holes detected?
X-ray inspection and ultrasonic testing find internal defects that visual inspection misses. Process auditing and per-batch records catch the drift that produces them in the first place.
Can pouring temperature really cause defects?
Yes. Pouring temperature and pouring speed that are too high or too low, too fast or too slow, promote both gas holes and sand holes. The parameters have to be held in range and monitored, not just set once.
Need castings produced to your drawing?
Hebei Yuanpeng Machine Tool and Measuring Implement Co., Ltd. has produced machine tool castings, measuring tools and cast iron surface plates since 1995. We hold the national plate measuring tool production licence and were among the first in the industry to obtain ISO 9001 certification. Our products are exported to the United States, Europe, Japan, South Korea and other markets.
Send your drawing, material specification and quantity to yuanpeng@yepoweldingtables.com, or use the enquiry form on our contact page. We reply within one working day.
Related products: Cast iron platform series · High precision flat cast iron plate · T-slot cast iron platform
Previous Page:

Contact Us
E-mail:
yuanpeng@yepoweldingtables.com
Service Hotline:
+86-19933786909
Address:
Industrial Development Zone, Jiaohe Town, Botou City
Sales Hotline: +86-19933786909
E-Mail: yuanpeng@yepoweldingtables.com
Address: (Hebei Province, China) Jianshe Road, Jiaohe Town, Botou City, Cangzhou City, Hebei Province


INQUIRY